The Question Behind the Question
Most buyers ask “hydraulic or electric servo press brake?” — wrong starting point. The right question is: what thickness range, what material mix, what daily bend count, and what tolerance does your downstream welding or assembly actually demand?
Hydraulic still dominates heavy plate work above 6 mm. Electric servo (and hybrid electro-hydraulic servo) owns the precision sheet metal space below 4 mm. The 3 mm to 6 mm crossover is where buying decisions get expensive and where sales talk gets slippery.
Twenty years of standing next to operators, watching machines leak oil at 2 AM, and arguing with procurement over energy bills — this is what I want to walk you through.
Hydraulic Press Brakes: The Honest Take
The hydraulic press brake is the diesel engine of sheet metal — heavy, reliable when maintained, expensive to keep running, but nobody questions whether it can do the work.
Where it wins:
- Tonnage. Need 400 tons for 10 mm cold-rolled steel? Hydraulic is still the default. Above 200 tons, fully electric becomes exotic and expensive.
- Peak load forgiveness. Hit a hard spot in thick plate or bend a section with grain variation, the hydraulic circuit absorbs the shock. Electric reacts faster, but that reaction shows up as tooling chatter or position drift on tough materials.
- Universal repair. Every decent factory has a mechanic who can change seals, top up oil, replace a hose. Parts are off-the-shelf. You can keep a 15-year-old machine running.
Where it costs you:
- Oil. A 100-ton press brake holds 100–250 L of hydraulic oil; larger machines exceed 400 L. Skip the change schedule and you learn about it through a proportional valve failure at ¥18,000 in parts plus two days of downtime.
- Idle energy. The motor on a 100-ton hydraulic draws 7.5–15 kW continuously when the machine is just sitting there powered on. Across a single-shift year (250 days), that’s 13,000–26,000 kWh — roughly ¥10,000–¥25,000 per machine, doing nothing.
- Heat. Hot oil (50–60 °C and climbing) means thinner oil, slower response, accelerated seal wear. Air conditioning the workshop to keep the press brake happy is a real cost.
Electric Servo Press Brakes: Where the Brochure Stops Being Honest
Energy efficient. Precise. Quiet. Clean. Half the truth.
Where it actually wins:
- Energy. The motor only draws significant current during the bend stroke. Idle power drops to near zero. On a real shop floor comparison I’ve tracked, an electric 80-ton consumed 30–50 % less electricity than a hydraulic equivalent on the same job mix. Over five years, that’s a meaningful number.
- Cycle speed. Servo-driven ram recovers faster between strokes. High-mix sheet metal shops running 200–800 bends per shift typically see 15–25 % cycle time reduction on parts below 3 mm.
- Positioning. Electric backgauges repeat to ±0.01 mm. Hydraulic backgauges typically repeat to ±0.03 mm or worse depending on age. For control panels, server racks, anything with tight bend-to-bend dimensions, this matters.
- Less routine maintenance. No oil changes, no seals, no hoses. Servo motors, encoders, drive electronics — done right, they last 8–10 years between major service.
Where the sales pitch lies:
- “No maintenance” is the lie. Electric systems need different maintenance, not less. When an encoder fails, the replacement is specific, expensive, and often needs a brand-certified technician. A hydraulic encoder failure is a mechanical replacement you can do with hand tools.
- Tonnage ceiling. Fully electric press brakes top out around 200 tons. Hybrid systems extend to about 400 tons. Above that, hydraulic still rules. Buyers eyeing electric machines for 6 mm+ structural work are usually buying the wrong machine.
- Environmental sensitivity. Drive electronics hate dust, humidity, and voltage fluctuation. In a dirty workshop with unstable power, the electric machine will have more downtime than the hydraulic one. The opposite of the brochure.
The Comparison That Actually Matters
| Parameter | Hydraulic | Electric Servo / Hybrid |
| Tonnage range | 30 – 2000+ tons | 20 – 400 tons |
| Idle energy | 7.5 – 15 kW continuous | < 1 kW standby |
| Per-cycle energy | High, motor runs constantly | 30 – 50 % lower |
| Position repeatability | ±0.03 mm typical | ±0.01 mm typical |
| Cycle rate | Slower recovery | 15 – 25 % faster on thin gauge |
| Maintenance cadence | Seal / oil / filter every 6–12 months | Annual inspection, 5+ years major |
| Common failures | Seal leaks, valves, pump wear | Encoder, drive electronics, bearings |
| Repair cost per incident | Low to medium, generic parts | Higher, brand-specific parts |
| Workshop requirements | Ventilation, oil containment | Clean power, dust control |
| 5-year TCO (100-ton class) | Lower upfront, higher operating | Higher upfront (~20–40 %), lower operating |
| Best fit | Thick plate > 6 mm, heavy structural | Thin to medium < 4 mm, precision |
A Real Factory Case
A sheet metal shop in eastern China — call them Factory X — ran three hydraulic 100-ton press brakes on two shifts. Energy bill for those three machines: roughly ¥180,000 per year. Two of the three had chronic seal issues. Average unplanned downtime: 4 hours per machine per month.
They replaced one machine with an 80-ton electric servo press brake. Same operator. Same parts. Same shift pattern.
Year 1 results on that single machine:
- Energy draw: ~60 % lower
- Unplanned downtime: under 1 hour per month
- Cycle time: 18 % faster on the same parts
- Maintenance cost: ¥8,000 vs ¥22,000 on the hydraulic units
Net Year 1 savings: ¥70,000–¥90,000.
But the other two hydraulic machines stayed, because the work mix included 6 mm and 8 mm stainless steel panels the electric machine couldn’t handle at the required tonnage. The factory ended up running a hybrid fleet — electric for precision thin gauge, hydraulic for heavy structural — and that mix is now their standard.
Lesson: this is rarely a “replace all” decision. It’s a “match the machine to the work” decision.
What Sales Don’t Quote
Tooling crossover. Electric machines expose tooling wear that hydraulic machines mask. Switching often reveals punches and dies you didn’t know needed replacement.
Skill gap. Electric servo needs people who understand drive electronics and encoder alignment. That skill is scarce and costs more than a hydraulic mechanic.
Spare parts. Hydraulic parts are universal, next-day delivery. Electric servo parts are often brand-specific, 1–4 week lead time, and cost 10–100× more per item.
Downstream rework. A 0.5° off-angle bend on a hydraulic machine becomes a welding fitting problem, becomes a grinding time issue, becomes a finishing cost. None of this shows up in the press brake quote. For tight-tolerance welded assemblies, the accuracy improvement of electric servo often pays for the upgrade in 18–36 months through reduced rework alone.
FAQ
Q: Should I buy electric servo if my main work is 2 mm stainless panels? A simple working rule: for mild steel, ~4 tons per mm of thickness per meter of bend length. Stainless needs ~1.5× that. For 2 mm stainless up to 2 meters of bend, an 80-ton electric servo handles it with safety margin to spare. Energy and accuracy savings typically pay back the premium in 2–3 years at volume.
Q: What standards apply? ISO 12100 (general safety), EN 12622 (press brake, EU), ANSI B11.3 (US), GB 17120 (China). CE marking is required for the European market. Any machine without a Declaration of Conformity is a legal liability waiting to happen.
Q: How long do these machines actually last? A well-maintained hydraulic: 15–25 years (seals, pumps, valves wear; the frame doesn’t). A well-maintained electric servo: 12–20 years, with drive electronics and servo motors as the typical mid-life replacement.
Q: Is compressed air really required? Yes — 6 bar (0.6 MPa) clean, dry air for upper-tool clamping and backgauge finger positioning. Skip the air dryer and water in the pneumatic system corrodes tooling clamps. Small investment, constant headache avoided.
Final Thought
The hydraulic-versus-electric press brake decision is not a technology choice. It’s a work-mix choice.
Heavy work, loose tolerances, long shifts, uncontrolled workshop climate — hydraulic still wins. The tech is mature, parts are universal, mechanics are available, and the machine runs for two decades.
Precision sheet metal, tight tolerances, small-to-medium batches, trained operators — electric servo or hybrid pays back the premium. Energy savings are real. Accuracy is real. Maintenance reduction is real.
Work crosses both — and most factories do — run a mixed fleet. Match the machine to the work, not the work to the machine.
The supplier who quotes you one machine for everything is selling you a compromise. The supplier who asks about your work mix, tolerances, shift pattern, and existing skills is the one worth listening to.
Want a Press Brake Configuration That Actually Fits Your Work Mix?
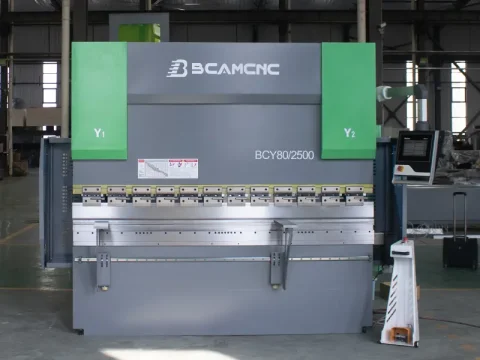
BCAMCNC has been building press brake systems, laser cutting equipment, and sheet metal fabrication lines for industrial customers for years. We don’t sell one machine for every job.
Tell us your work mix — thickness, material, tolerance, batch size, downstream process — and we’ll configure the tonnage, bed length, control system, and backgauge axes around what actually runs on your floor. No template quote. No upsell on axes you won’t use.